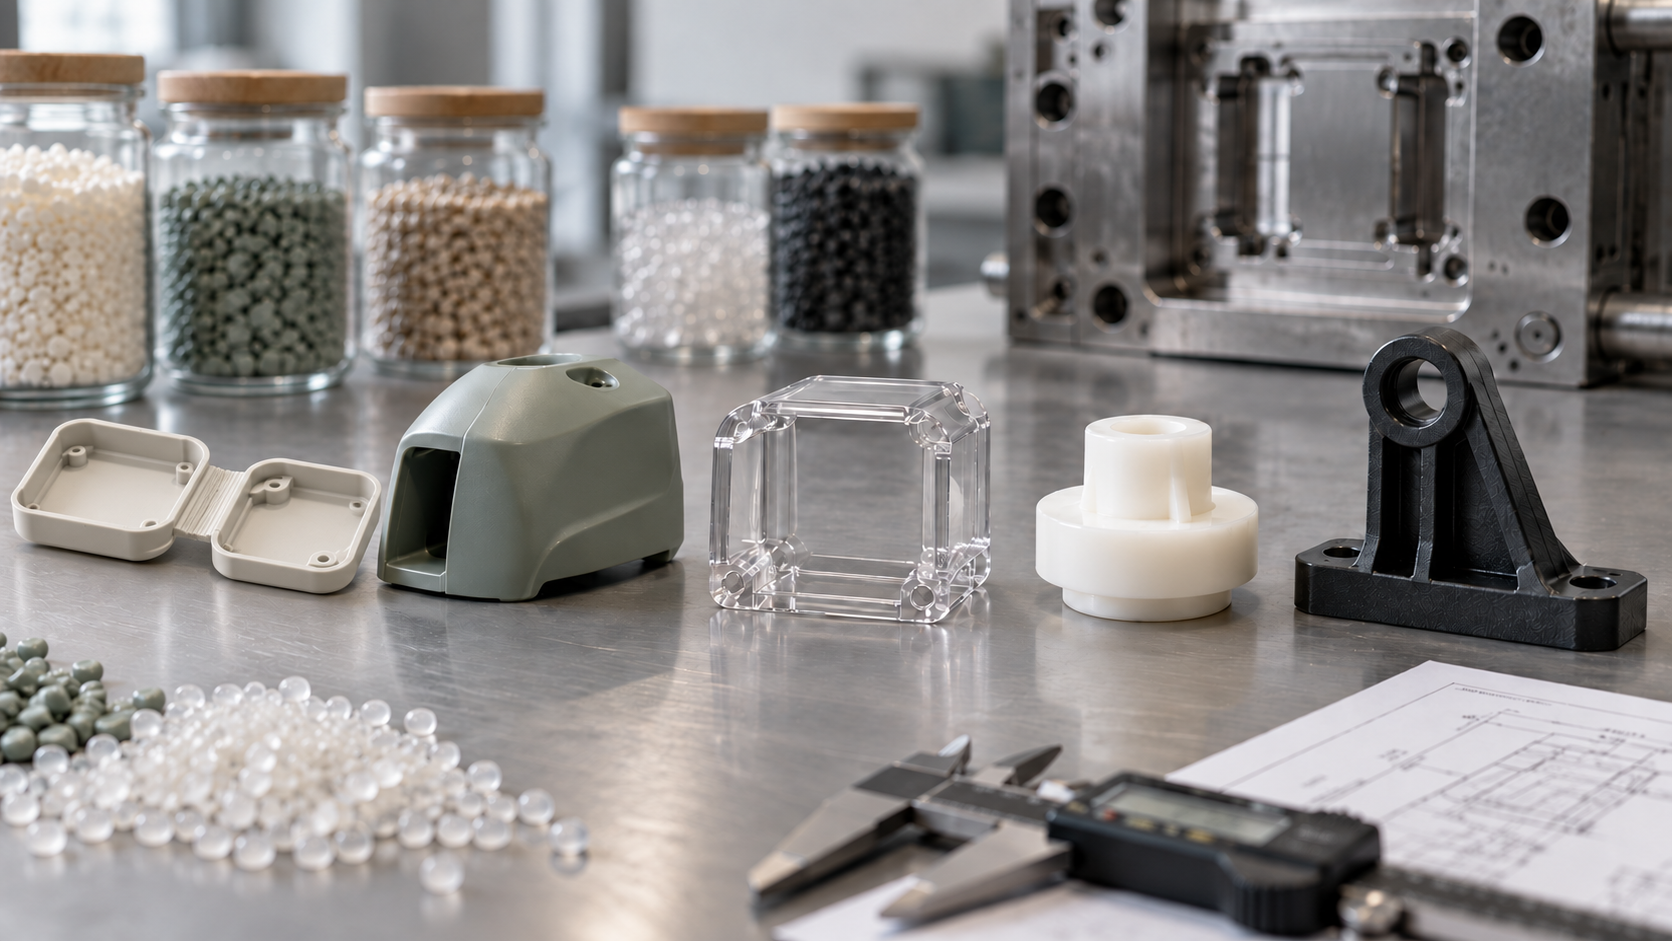
The cheapest resin on the quote is not always the cheapest material for the finished product. Pick a polymer on piece price alone and the bill can arrive later in the programme: warpage, dimensional change, cosmetic defects, poor durability or early failure. Any one of those can cost far more than the material saving.
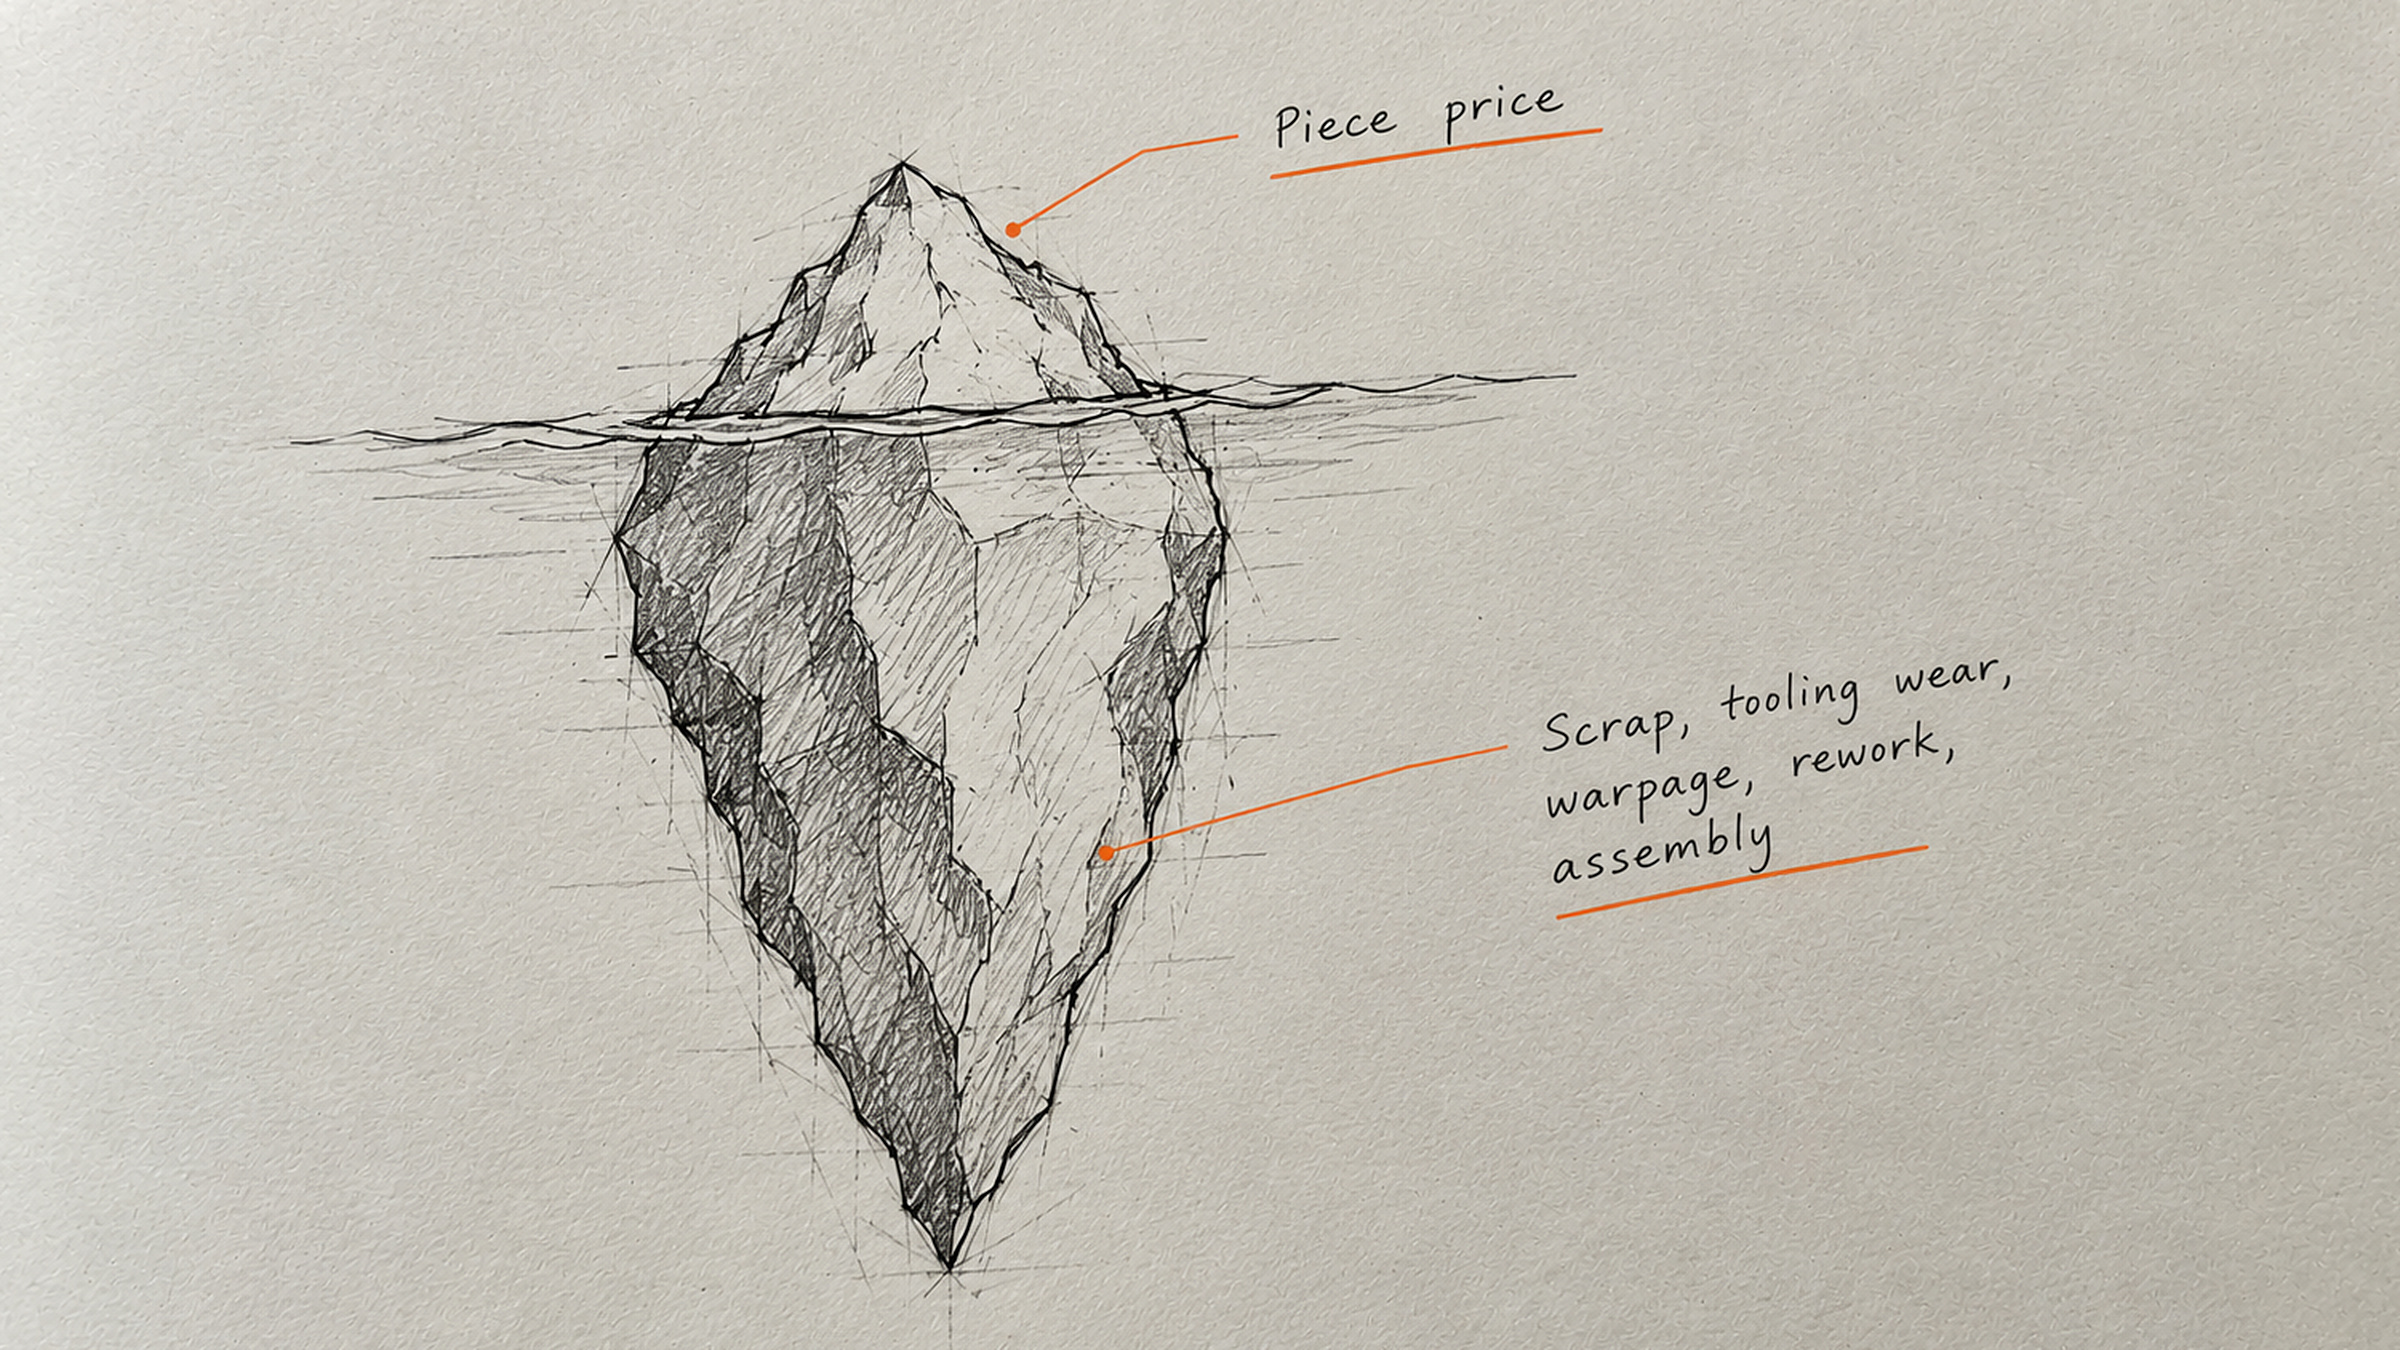
The piece price is the tip. Scrap, tooling wear, warpage, rework and assembly sit below the waterline.
We always start with the datasheet, but we never stop there. A datasheet tells you how a grade performs under defined laboratory conditions. It does not tell you how that grade will behave in your tool, with your part geometry, processing conditions, surface finish and end environment. So we look at the part, the process and the end use together.
Where material selection can go wrong
Every polymer family and grade has its strengths and its limits. The table sets out five common families side by side. The notes after it cover the points we check most carefully, because they are the ones that most often catch people out.
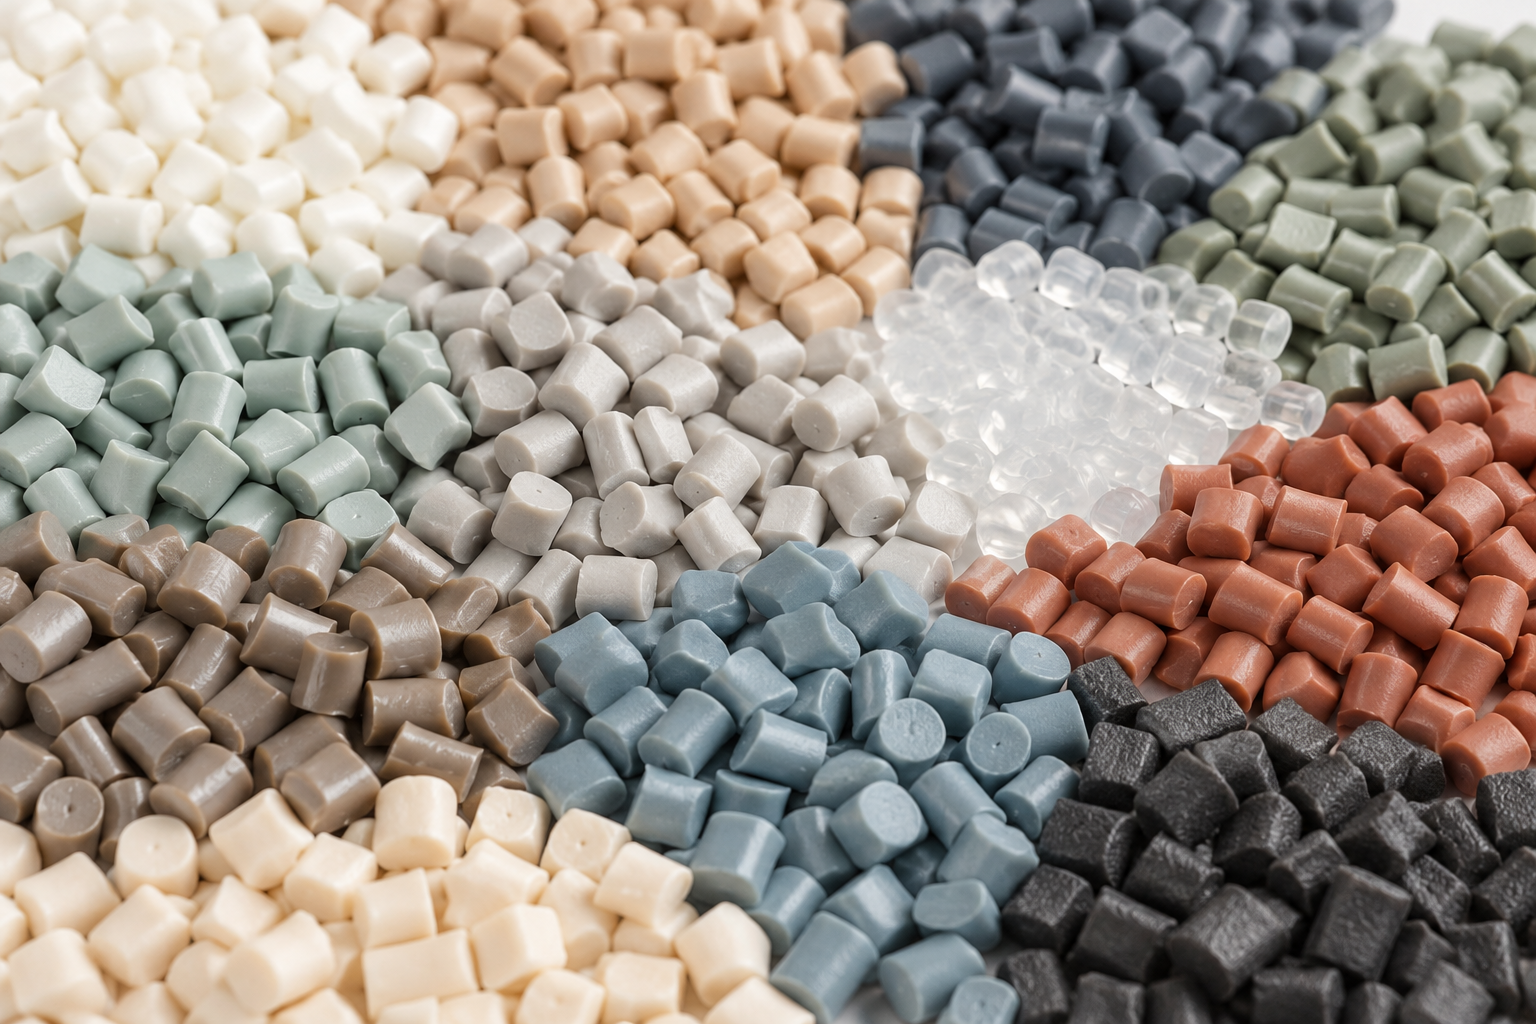
Resin starts as pellets. Grade, stabilisation and process decide how that material behaves in the tool and in the field.
| Polymer | Strengths | Watch out for | Typical uses |
|---|---|---|---|
| ABS | Relatively easy to process; good surface quality | Standard grades may not suit prolonged outdoor or UV exposure without appropriate stabilisation | Enclosures, housings and cosmetic parts used indoors |
| Nylon (PA) | Excellent strength and stiffness | Absorbs moisture, which can change both mechanical properties and dimensions after moulding | Clips, snap fits, gears and structural parts, with moisture planned for |
| Polypropylene (PP) | Living hinges, chemical resistance, low density | Homopolymer, random copolymer and impact copolymer grades behave differently, especially in a living hinge | Living hinges, lids and lightweight, chemically resistant parts |
| Polycarbonate (PC) | High impact strength; can be transparent | Sensitive to moisture during processing and needs appropriate drying | Demanding applications, including transparent components |
| POM (acetal) | Low friction, wear resistance, dimensional stability | The right grade still depends on load, temperature, chemicals and wear; UV-stabilised grades exist for outdoor use | Gears, sliders and other moving or wearing parts |
Nylon is the one we watch most closely. A dimension that measures correctly on a freshly moulded part can move as the material reaches equilibrium with its environment. On clips, snap fits, gears and precision interfaces that matters, because dimensional stability is the whole point of the part.
Polypropylene shows why we specify the grade, not just the family. PP is an excellent choice for living hinges, chemical resistance and low-density parts, but homopolymer, random copolymer and impact copolymer grades can behave differently, especially in a living hinge. We pin down the grade before the hinge design is finalised.
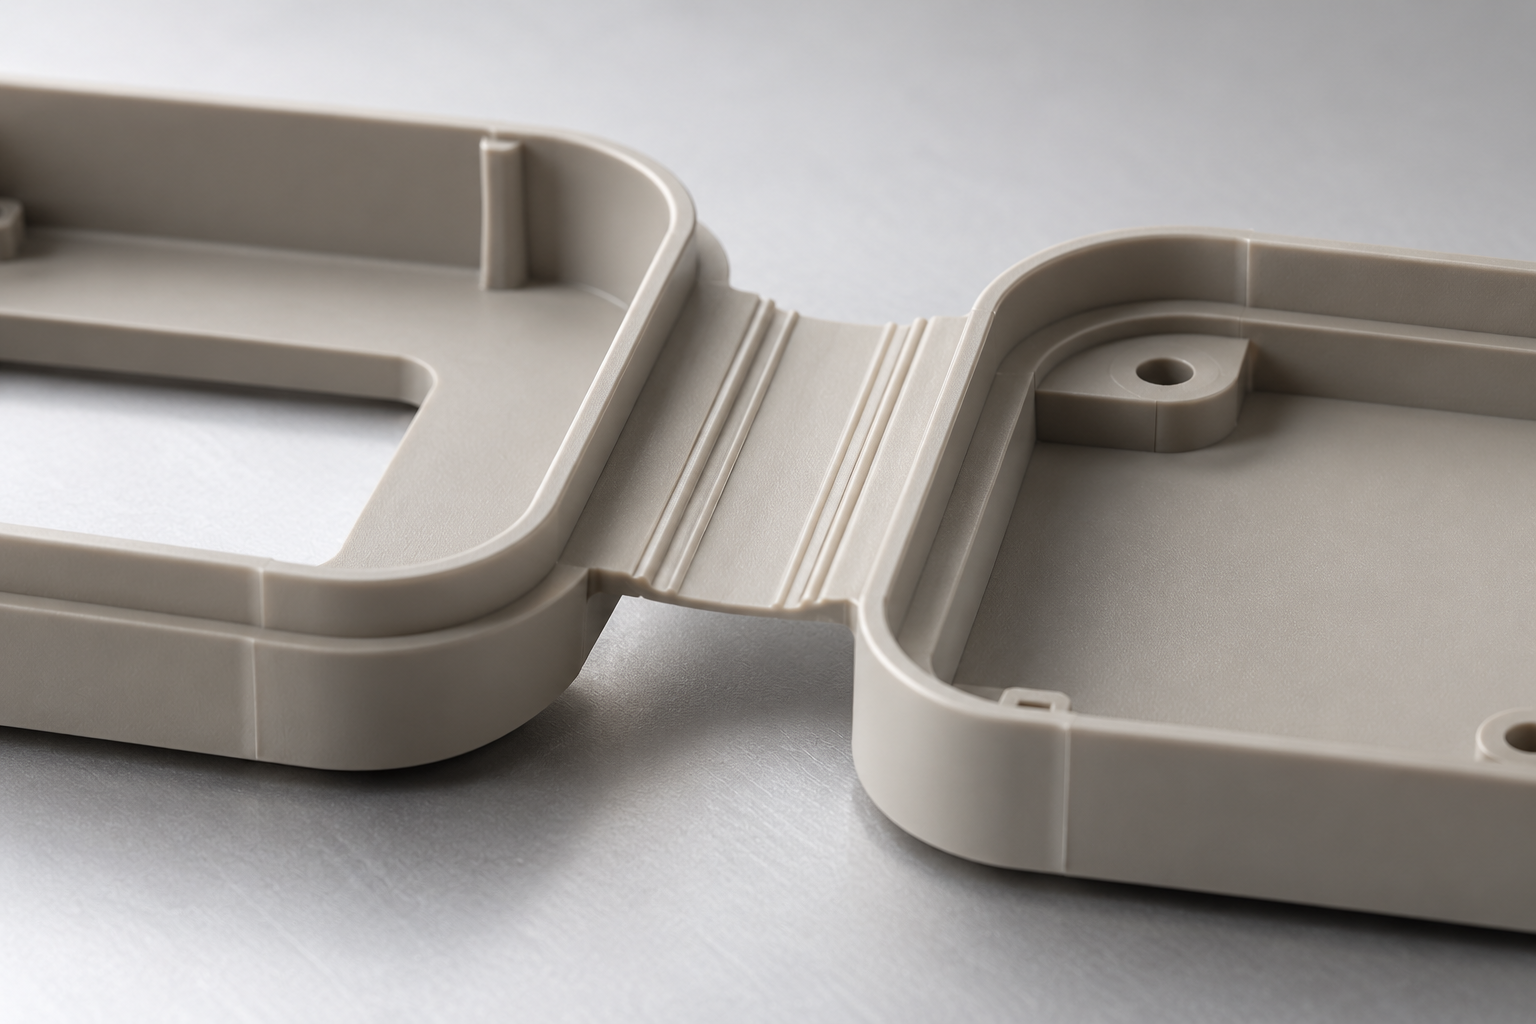
Living hinges depend on the right PP grade. Homopolymer, random copolymer and impact copolymer are not interchangeable.
Glass-filled materials
Glass fibre is extremely useful when you need extra stiffness, strength or dimensional stability. It also brings new things to manage. Fibre orientation can influence shrinkage, warpage and mechanical performance, and the fibre content that improves structural performance can also affect surface appearance and tool wear.
That does not make glass-filled materials a bad choice. It means we select them with the geometry, tooling, cosmetics and load path in mind.
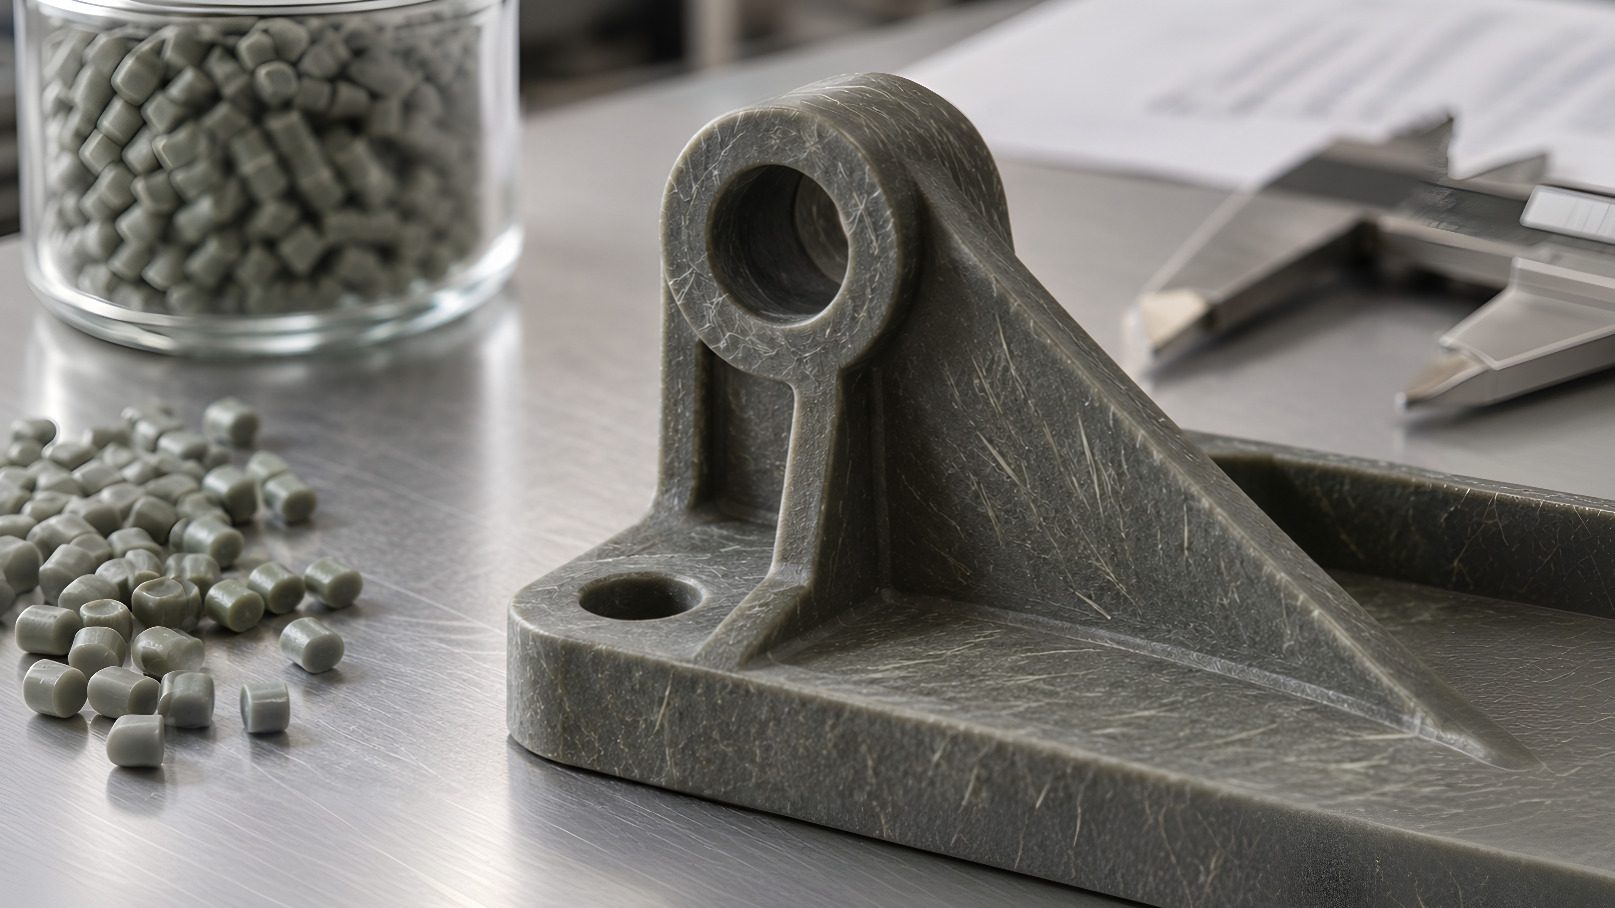
Glass fibre can add stiffness and strength, but fibre orientation and content also affect surface appearance and tool wear.
Material selection should start with the application
Before we talk grades, we ask what the finished part has to survive. These are the questions we work through first.
- Indoor or outdoor use?
- Exposure to UV?
- Repeated loads or impacts?
- Contact with chemicals or cleaning products?
- Repeated flexing?
- High or low operating temperatures?
- A cosmetic or highly visible surface?
- Tight dimensions that must hold over time?
Once we have those answers, we choose the material family and then the specific grade. Bear in mind that “ABS”, “PP” or “PA66” is not a complete material specification. The exact grade, reinforcement, stabilisation package, colour and other formulation details can all affect the finished part and how we need to process it.
Prove the material before cutting steel
We want the production material decided early enough to shape the design and tooling decisions. If mould-flow or warpage analysis is being run, we would rather it used the intended production grade than a generic material with similar headline properties.
We also assess critical dimensions in the condition your customer will actually use the product. For moisture-sensitive materials such as nylon, that can mean conditioning parts before the final dimensional check.
Our aim is not the cheapest material. It is the right material for the product, the process and the application, proven before significant tooling cost is committed.
Piece price is only one part of the cost
Material price always matters, but it is only one line in the manufacturing cost. Processing window, cycle time, scrap, tool wear, cosmetic performance, assembly yield, product reliability and field failures can all have a much greater impact on what the product finally costs you.
Indicative, not to scale. The resin price is the visible part of the cost. The blocks above it can have a much greater impact, and their size varies by part and programme.
A material that costs slightly more per part can be the more economical choice if it gives you a more robust, repeatable and reliable product. The cheapest resin is not always the lowest-cost answer.