A production delay rarely costs just the revenue you lose while you wait. When we cost one properly, it runs through the whole business.
On a project plan, a three-month delay looks simple. Move the production date, move the launch date, move the customer delivery. In reality it is rarely that tidy.
A late production run can hit inventory, cash flow, customer commitments, marketing activity, assembly capacity, freight, supplier relationships and the next project already waiting for the same resources. The longer it runs, the harder it is to recover.
Where production delays really start
Delays rarely come out of nowhere. When we trace one back, it usually started much earlier in development, with one of these:
- A design is not fully ready when tooling begins.
- A critical material has not been properly validated.
- Tool modifications are underestimated.
- T1 issues are accepted rather than fully resolved.
- A supplier cannot achieve the required cycle time or quality.
- Production capacity has not been secured.
- A component is dependent on another supplier who is already behind schedule.
None of these looks like a three-month problem on day one. A few days for a design change. A week for a tool modification. Another sample run, a late material shipment, a missed production slot. Each one looks manageable. Together, they can quickly eat the programme.
Indicative, not to scale. Each slip looks small on its own. Stacked end to end, they become the delay.
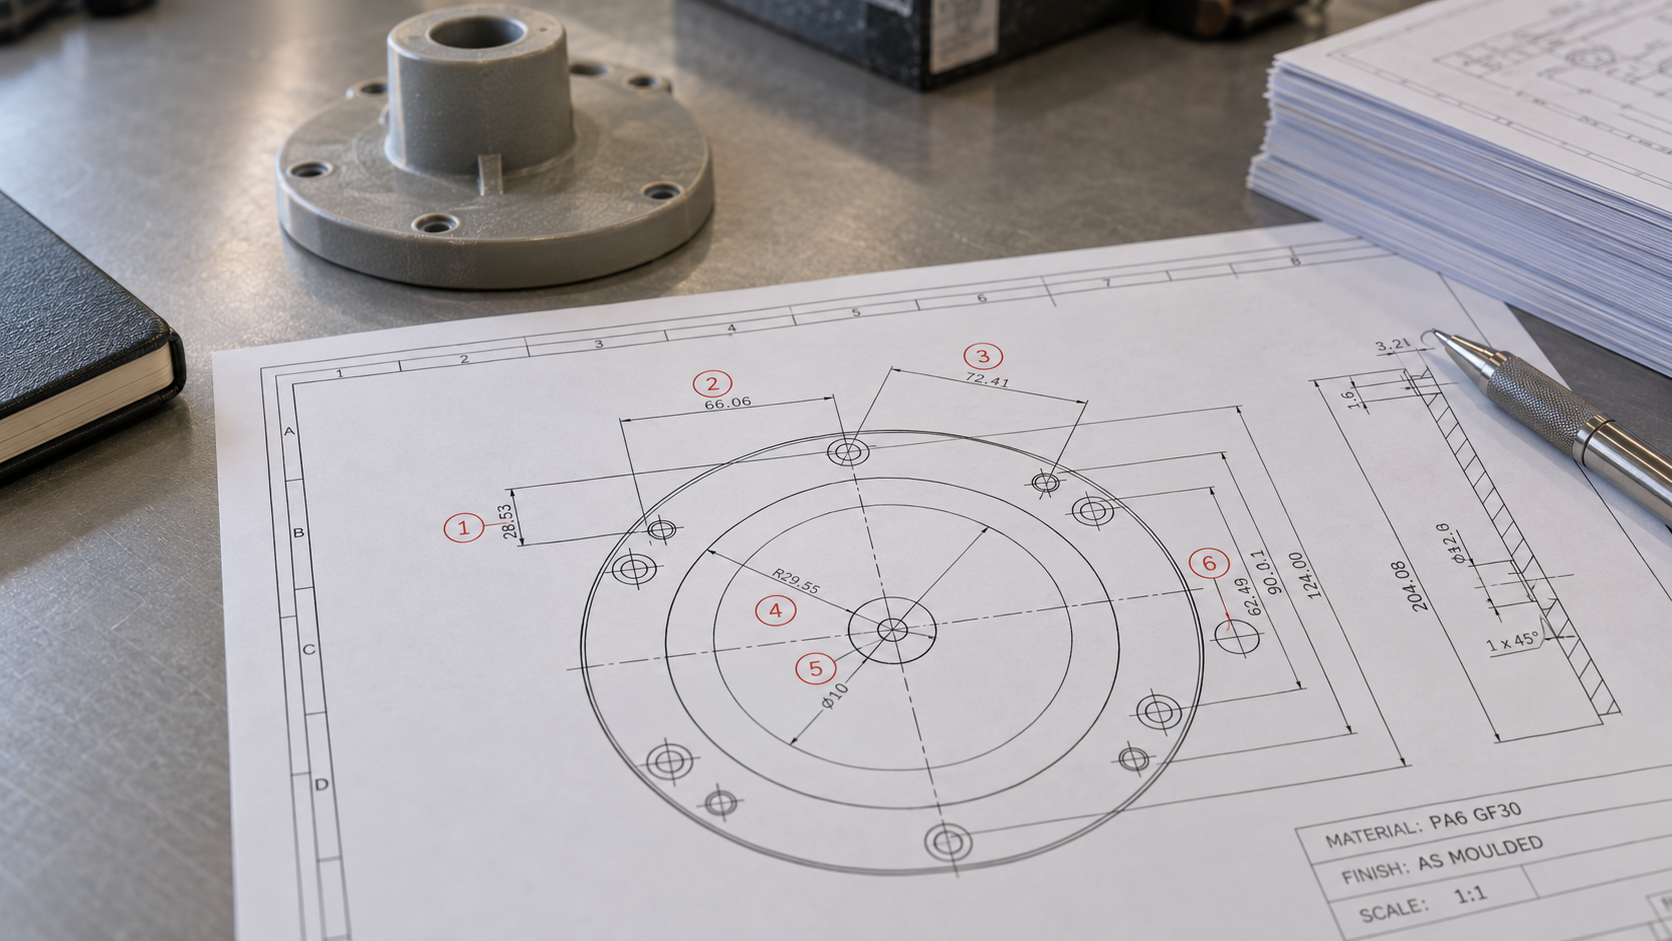
Early decisions on design readiness, materials and inspection gates often decide whether a small slip stays small.
The hidden cost of waiting
Lost production is the obvious cost. We look for the others running in parallel, because most of them never appear on the project plan.
Parts that are made but not shipped are cash tied up while you wait.
| Cost | What happens | Where it shows up |
|---|---|---|
| Revenue | If the product cannot be manufactured, it cannot be shipped. With a fixed launch window, three months can mean missing a seasonal launch, customer commitment or market opportunity altogether. | Sales forecast and launch plan |
| Inventory and cash flow | Money already committed to tooling, development, materials and components sits in the supply chain rather than generating finished products, while other costs continue to build. | Cash flow and stock held |
| Expedited recovery | Air freight instead of sea freight, overtime, additional tooling work, expedited materials, extra inspection and additional shifts. Sometimes unavoidable, rarely in the original business case. | Freight, overtime and supplier invoices |
| Assembly and downstream | If the product needs ten parts and one is missing, the other nine may simply be waiting. Assembly capacity is left unused, parts are stored for longer and planning moves around the problem. | Assembly capacity, storage and the production schedule |
| Customer confidence | Customers, retailers, sales teams and marketing all plan around the date. Once it has been missed, rebuilding confidence can take much longer than recovering the schedule. | Customer relationships and future orders |
Of the five, customer confidence is the hardest to put a number on. A missed delivery date can do more damage than the direct financial cost, because customers plan around commitments, retailers plan launches and sales teams make promises based on availability.
The problem with recovering time
The biggest mistake we see in plans is assuming a three-month delay can be won back by asking everyone to work faster. Sometimes it can. Often it cannot.
If the tooling needs another modification, the toolmaker still needs to make the change. If a material needs to be ordered, there is still a lead time. If the production slot has been lost, another supplier may already be committed. And if testing has been compressed, you may simply be moving the risk further downstream.
This is where a small delay gets expensive. Corners get cut to recover time, and the cost of those decisions may only show up later as quality issues, rework or field failures.
The cheapest time to fix a problem
The earlier we find a manufacturing risk, the more options you have. A design change before tooling can be relatively straightforward. The same change after steel has been cut may require a tool modification. After T1, it may require another trial. After production has started, it may mean rework, scrap or a change to an already-established process. And once products are in the hands of customers, the options become considerably more expensive.
Indicative, not to scale. The same change gets harder and more expensive at every stage it slips past.
That is why we do not treat manufacturing as something that happens after the design is finished. We want material, process, tooling, tolerances, assembly and production requirements on the table early enough to shape the design.
Building time into the right places
A good programme is not about adding more time everywhere. It is about knowing where the real risks are and making the schedule reflect them. When we review a plan, we look for time set aside for:
- Proper DFM review before tooling.
- Tool design and manufacturing.
- T1 sampling and process development.
- Tool modifications where required.
- Material validation.
- Dimensional and functional testing.
- Production approval.
- Supplier capacity and lead times.
- Final assembly and quality inspection.
We are not trying to make every programme longer. We are trying to stop anyone pretending the risky parts will go perfectly first time.
The real cost of a delay
So a three-month delay is much more than three months of lost time. It can mean lost revenue, additional freight, wasted capacity, inventory costs, engineering time, tooling modifications, rework and damaged customer relationships.
The frustrating part is that many of these costs are created long before anyone officially calls it a delay. The best time to manage production risk is before it becomes a production problem.